Introduction
Two of the most common ways to move material in a cement plant are the belt conveyor and the air slide. Both move bulk material reliably — but they are built for different jobs. A belt conveyor carries granular and lumpy material over long distances, up and down slopes. An air slide fluidizes fine powder with low-pressure air and lets it flow downhill on a cushion of air.
Choosing between them is not about which is “better” — it is about matching the machine to the material and the route. Pick wrong and you pay for it in dust, wear, energy, and maintenance for years. This guide compares the two side by side and gives a step-by-step decision framework for cement plant engineers.
1. The Short Answer
- Use an air slidefor dry, fine, free-flowing powder (cement, raw meal, fly ash) over short to medium distances (typically up to 60-100 m) with a downward slope available.
- Use a belt conveyorfor granular or lumpy material (clinker, limestone, additives), long distances, and routes with rises or changes in elevation.
- Both exist in most cement plants— the question is never “which do we standardize on,” but “which fits this specific transfer.”
2. How Each Machine Works
2.1 How an air slide works
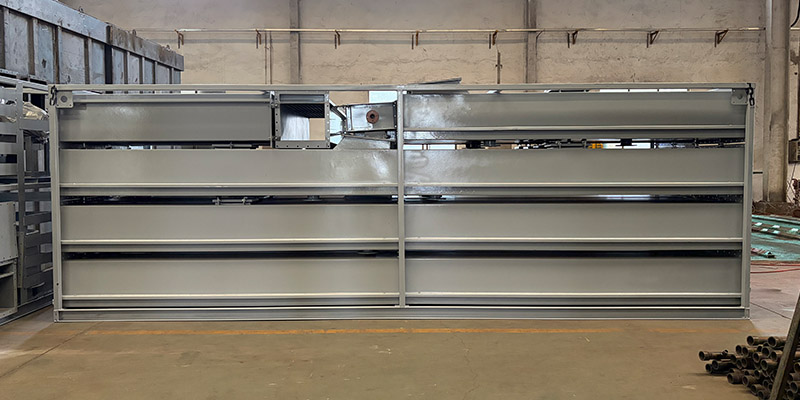
An air slide is a downward-inclined enclosed trough (typically 4-8° slope) with a porous fabric or membrane across the middle. Low-pressure air (typically 0.4-1.0 kPa) is blown into the chamber below the fabric; the air passes up through the porous layer and fluidizes the powder above it. Fluidized powder behaves almost like a liquid — it flows downhill through the upper chamber with very little slope, at high rates, with no moving parts in contact with the material.
Key characteristics:
- Only fine, dry, free-flowing powders can be fluidized
- Requires a downward slope — cannot lift material
- Requires a continuous low-pressure air supply (blower)
- No moving parts in the material path — very low wear
- Fully enclosed — no dust escape, no spillage
2.2 How a belt conveyor works
A belt conveyor is a continuous loop of rubber (or fabric/steel-cord) belting running over idler rollers, driven by a head pulley and tensioned at the tail. Material rides on top of the belt and moves with it. Standard troughed idlers give the belt a U-shape that carries more material with less spillage.
Key characteristics:
- Handles granular, lumpy, and abrasive material — and powder too
- Transports horizontally, on slopes (up to 15-20° for standard troughed belts, more with special belt designs), and over long distances (kilometers possible)
- Moving parts in the material path: belt, idlers, pulleys — wear and maintenance are real costs
- Requires transfer points, skirts, and dust control at loading/unloading points
- Higher investment and running cost than an air slide for short powder runs

3. Side-by-Side Comparison
| Factor | Air slide | Belt conveyor |
| Material type | Fine dry powder only | Granular, lumpy, powder |
| Max typical distance | 60-100 m | Kilometers |
| Slope | Downhill only (4-8°) | Horizontal, up to 15-20°+ |
| Lift capability | No | Yes |
| Air/power | Needs low-pressure blower | Drive motor only |
| Dust control | Fully enclosed, no dust | Dust at transfer points; needs covers/hoods |
| Moving parts in material path | None | Belt, idlers, pulleys |
| Wear rate | Very low | Moderate to high (abrasive material) |
| Maintenance | Low (fabric, blower) | Higher (belt tracking, idlers, rollers) |
| Investment (short powder run) | Lower | Higher |
| Noise | Low | Moderate (idlers, drives) |
4. Decision Framework: Step by Step
Step 1 — What is the material?
- Fine, dry, free-flowing powder → air slide is a strong candidate
- Granular, lumpy, abrasive, wet, or sticky → belt conveyor
- Powder but not free-flowing (cohesive, high moisture) → air slide may not fluidize reliably; belt or screw conveyor instead
Step 2 — What is the route?
- Downhill or level with small slope → air slide possible
- Horizontal without slope → air slide still works (with slightly higher slope or air pressure), but belt is often simpler
- Any rise or elevation gain → belt conveyor (or elevator)
Step 3 — What distance?
- Up to ~60-100 m → air slide competitive on cost and maintenance
- Longer than 100 m → belt conveyor economics improve; air slide needs multi-stage or becomes costly
Step 4 — What are the constraints?
- Dust emission limits strict? → air slide wins (fully enclosed)
- Compressed/low-pressure air available? → air slide needs a reliable blower
- Space? → air slide is a slim trough; belt needs width plus head/tail space
- Maintenance staff available? → belt conveyor needs more routine attention (tracking, idlers, rollers)
Step 5 — Lifecycle cost
Compare investment + energy + maintenance + downtime over 10 years, not purchase price. For a short powder run, the air slide usually wins. For a long or lifting route, the belt conveyor is the only practical choice.
5. Cement Plant Application Examples
| Application | Typical choice | Why |
| Mill discharge → bucket elevator / silo (cement, raw meal) | Air slide | Short run, fine powder, fully enclosed |
| Silo to packing plant | Air slide or belt | Short distance, powder — air slide keeps it dust-free |
| Clinker storage to mill | Belt conveyor | Lumpy, abrasive, longer distance |
| Limestone crusher to raw mill | Belt conveyor | Large lumps, distance, elevation |
| Fly ash from collector to silo | Air slide | Fine powder, short run |
| Additives (gypsum, slag) to mill | Belt conveyor | Lumpy material |
The pattern: powder + short + no lift → air slide; lumps + long + lift → belt conveyor.
6. Common Mistakes to Avoid
| Mistake | Result | Fix |
| Air slide with coarse or wet material | Blockages, no fluidization | Check material first; belt for coarse/wet |
| Air slide without a slope | Material stops | Provide 4-8° slope or sufficient air |
| Belt conveyor for a 20 m powder transfer | Overkill cost, dust problems | Air slide instead |
| Ignoring belt maintenance (tracking, idlers) | Misalignment, belt damage, downtime | Scheduled belt maintenance routine |
| Undersized blower on an air slide | Poor fluidization, low capacity | Size blower for capacity + slope |
| No dust control at belt transfer points | Dust emissions, housekeeping | Covers, hoods, dust collection |
7. Quick Selection Table for Cement Plant Engineers
| Your case | Recommendation |
| Fine dry powder, short distance, slope available | Air slide |
| Fine dry powder, medium distance, no lift | Air slide (check length) |
| Granular/lumpy material, any distance | Belt conveyor |
| Any material, long distance (100 m+) | Belt conveyor |
| Any material, route with lift | Belt conveyor |
| Strict dust requirements, powder | Air slide |
| Abrasive lumps | Belt conveyor (with heavy-duty belt) |
8. FAQ
Q1: What is the maximum length of an air slide?
Typically 60-100 m in one run, depending on slope, material, and air pressure. Beyond that, belt conveyors usually become the better choice, or the air slide is split into stages.
Q2: Can an air slide transport material uphill?
No. An air slide needs a downward slope (typically 4-8°). For any lift, use a belt conveyor or a bucket elevator.
Q3: Which has lower maintenance, an air slide or a belt conveyor?
The air slide. It has no moving parts in the material path — just the fabric membrane and a blower. A belt conveyor has the belt, idlers, pulleys, and drives, all of which wear and need attention.
Q4: Can a belt conveyor handle fine powder like cement?
Yes, but it needs proper dust control (covers, transfer hoods, sometimes a dust collector) and skirt sealing. For short powder runs, an air slide is usually cleaner and cheaper.
Q5: What is the energy consumption difference?
An air slide needs a low-pressure blower running continuously; a belt conveyor needs a drive motor sized to load and distance. For short powder transfers, the air slide is typically lower in energy; for long or heavy-duty routes, the belt is more efficient per tonne.
Q6: Can an air slide handle raw meal or fly ash?
Yes — dry raw meal and fly ash are ideal air slide materials. They are fine, dry, and free-flowing when properly fluidized.
Q7: What slope does an air slide need?
Typically 4-8° for most cement powders. The required slope depends on material flowability and air pressure; more difficult powders need more slope or more air.
Q8: When should I definitely not use an air slide?
When the material is coarse, wet, sticky, or contains lumps, or when the route requires lifting. In those cases use a belt conveyor (or screw conveyor for short, contained runs).
9. Summary
The choice between air slide and belt conveyor is made by material, route, and distance:
- Material— fine dry powder → air slide candidate; granular/lumpy/wet → belt
- Route— any lift → belt; downhill/level → air slide possible
- Distance— up to ~100 m → air slide competitive; longer → belt
- Constraints— dust, air supply, space, and maintenance all tilt the decision
- Lifecycle cost— compare 10-year cost, not purchase price
Both machines have their place in every cement plant. Match the machine to the transfer and you cut dust, wear, and energy at the same time.
Need help selecting a conveying system? Contact Darko Cement. We manufacture air slides for powder handling and belt conveyors for granular and long-distance duty, and our engineers will match the right system to your material and route. Also comparing screw conveyors? See our screw conveyor vs belt conveyor guide.