

Integrated Material Handling & Dust Control Solutions for Continuous Cement Plant Production
Material handling and dust abatement systems for cement manufacturing must operate continuously against highly abrasive, dusty raw materials while maintaining stable, predictable performance. Darko designs integrated cement plant systems engineered to overcome these harsh operational challenges.
Our solutions span the full cement production workflow: quarry long-distance conveying, high-capacity vertical transport, raw material storage, cement grinding, silo discharge, dust collection, cement process valves and enclosed bulk loading for finished cement dispatch.
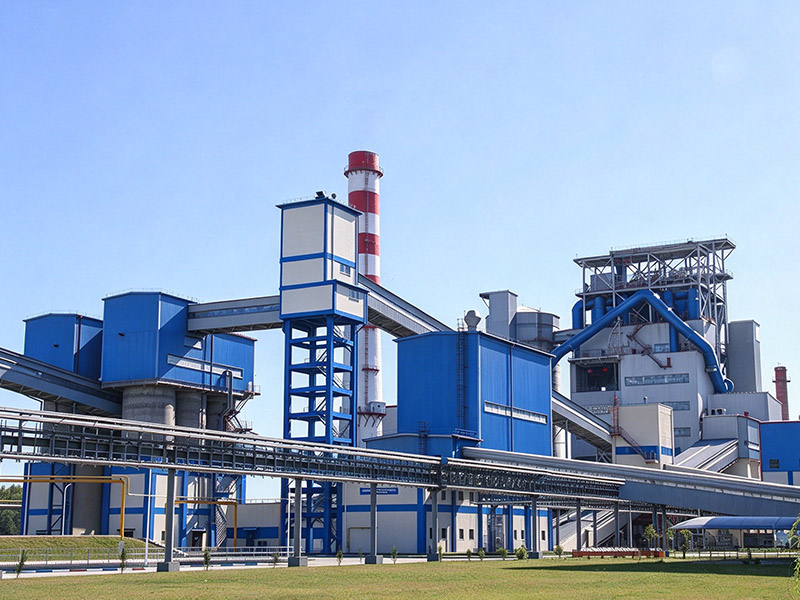
Durable Cement Handling Equipment for Higher Uptime
Our heavy-duty custom-engineered equipment handles limestone, raw meal, clinker and mineral additives, while managing dust at transfer and loading stations. Built for cement’s tough operating conditions, our solutions sustain consistent production, high throughput and on-time delivery targets.
Each subsystem optimises material flow, cuts routine maintenance work and lifts your overall plant productivity.
Handling Large Volumes at High Capacity
Efficient transportation of bulk raw materials is fundamental for cement production, starting at quarry excavation through raw meal preparation. Darko delivers high-capacity conveying solutions tailored to cement’s strict operational requirements. Our troughed belt conveyors are ideal for long-distance raw material transport from quarry to plant, even across uneven and challenging terrain. Within plant boundaries, our belt bucket elevators and complete in-plant conveying systems provide reliable vertical and horizontal transfer for raw meal, hot clinker, mineral additives and finished cement powder.
For alternative fuel (AFR) processing including shredded tyres, waste plastics and refuse-derived fuel (RDF), Darko provides complete AFR handling subsystems. From material receiving, stockpiling, precise dosing to fully enclosed conveying routes, our design enables safe, dust-free and cost-effective integration of alternative fuels into your cement kiln process.
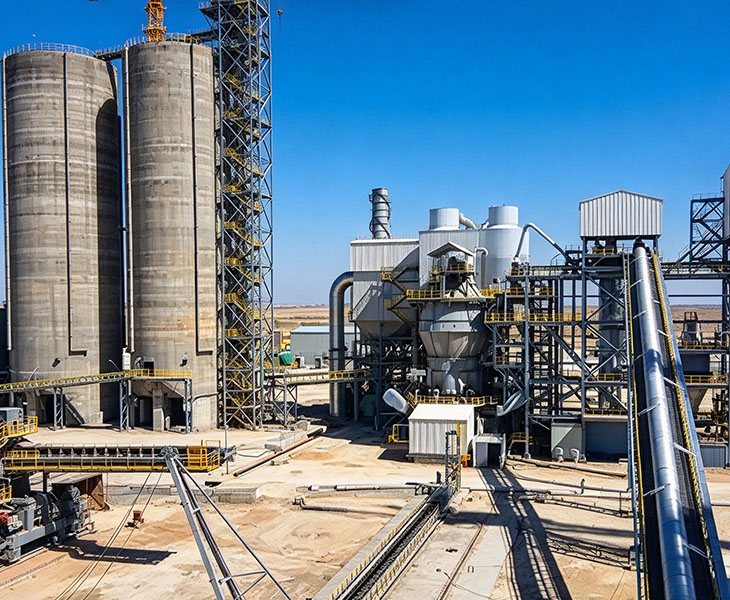
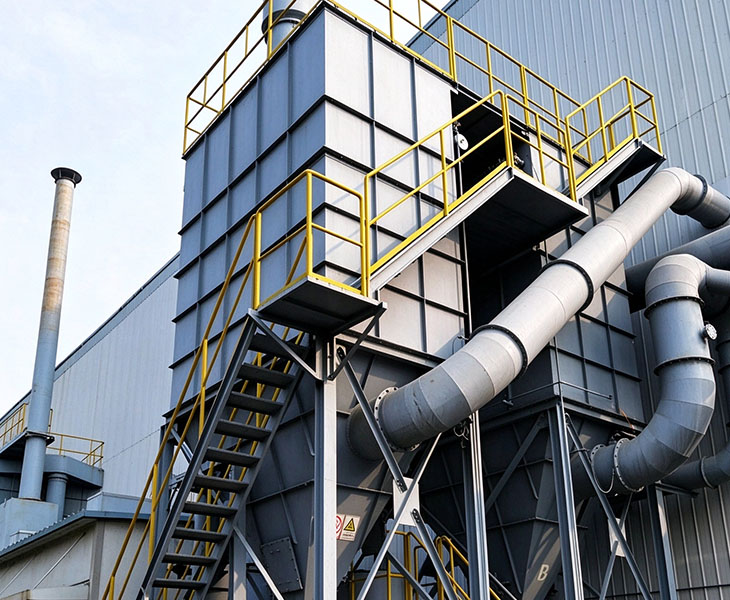
Fugitive Dust Control Across Cement Production Lines
Dust emission remains one of the most persistent operational headaches for cement facilities. Fugitive dust accumulates at kiln tail, raw mill, cement mill, transfer chutes, silo vents and bulk loading stations, risking regulatory penalties and worker safety issues. Darko’s cement dust control systems are engineered to capture fine particulate matter and help operators meet strict local environmental emission standards.
Our core equipment includes pulse jet baghouse filters, cartridge dust collectors, custom ductwork and extraction hoods. Each dust collection unit is selected according to gas temperature, dust concentration, particle characteristics and working conditions. The system protects plant personnel from dust exposure, reduces product loss and avoids environmental penalties.
We also provide retrofit services for outdated dust collection systems, including filter bag replacement, fan upgrade, duct re-design and pulse cleaning system optimisation to achieve ultra-low particulate emissions.
Dust‑Free Bulk Loading & Silo Discharge
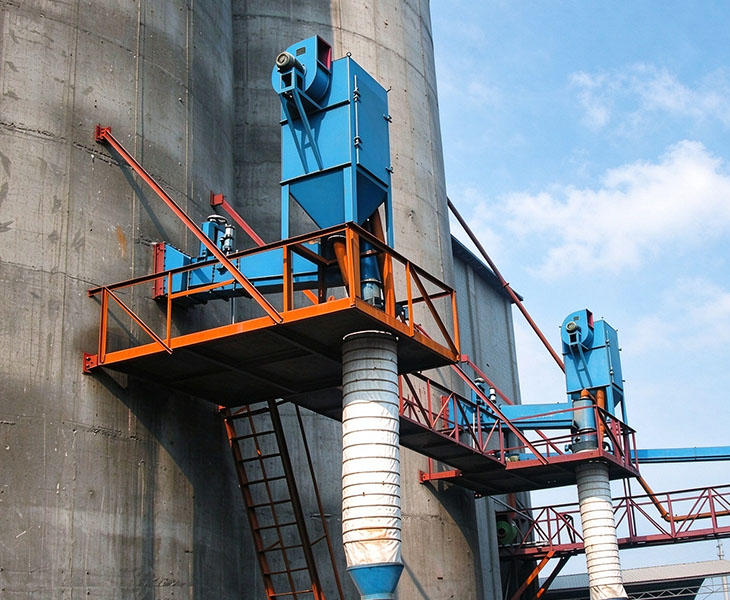
Cement powder and fine additives often suffer from silo arching, ratholing and unstable discharge. Unsealed bulk truck loading creates heavy fugitive dust and material waste. Darko supplies complete silo discharge assemblies and enclosed cement bulk loading systems.
Our silo aeration pads, air slides and flow control valves activate stagnant powder inside silos for consistent, uninterrupted material outflow. The automatic cement bulk loader forms a sealed connection between silo and tanker, eliminating dust escape during loading. This integrated solution improves loading speed, reduces cement waste and creates a cleaner working environment for loading bays.
Process Valves for Cement Process Lines
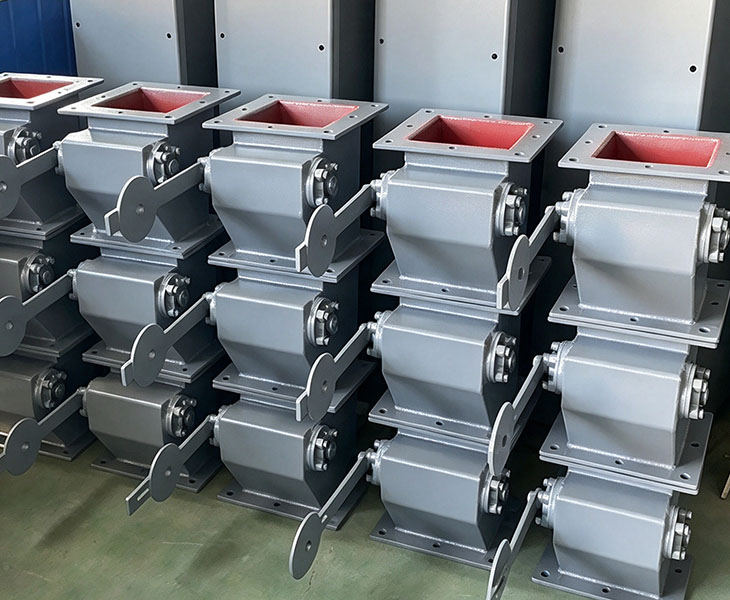
Cement production handles highly abrasive powders with frequent on-off cycling and fluctuating temperatures, imposing severe requirements on process valves. Darko supplies a full portfolio of cement-specific process valves for silo outlets, conveying pipelines, dust removal ash hoppers and material diversion points.
Our product range includes rotary air locks, slide gate valves, butterfly valves, diverter valves . All units feature anti-abrasion liners and heavy-duty sealing structures to withstand cement powder, raw meal and clinker dust.
These valves perform material cut-off, flow regulation and material switching. Manual, pneumatic and electric actuator options are available. Widely applied for raw material feeding, silo discharge, dust collector ash discharging and material diversion in cement plants. Custom wear-resistant upgrades are available for extreme abrasive working conditions.
Why Choose Darko for Your Cement Plant Project
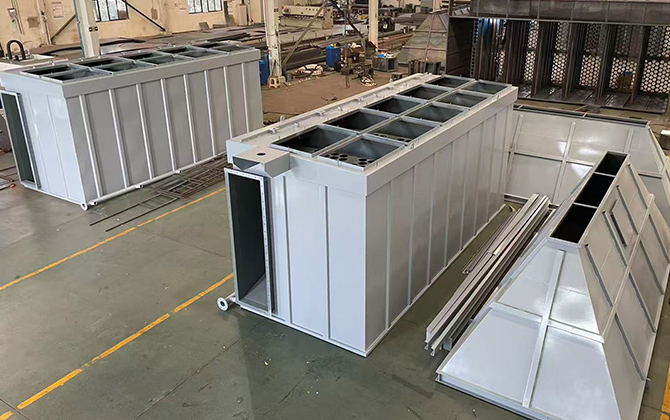
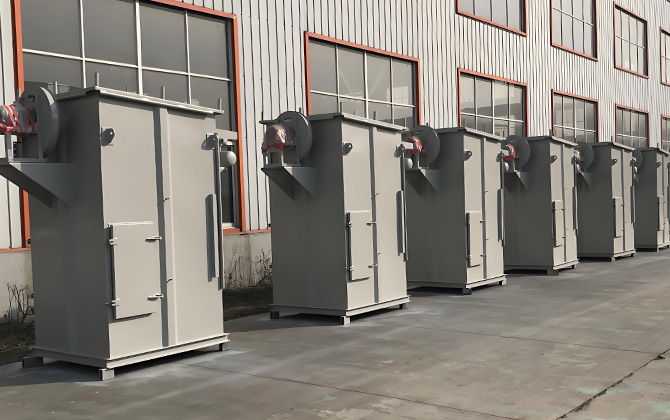
Darko balances premium international system quality and practical cost efficiency. We specialise in cement plant retrofits and new grinding line projects, with flexible lead times to support global cement projects across Southeast Asia, the Middle East and Africa.
Unlike many suppliers that only sell standalone machinery, our engineering team evaluates your full material workflow to ensure every subsystem works in harmony. We deliver equipment with heavy-duty wear protection and offer long-term spare parts support, reducing your plant’s total cost of ownership.
Custom-Built & Reliably Supported
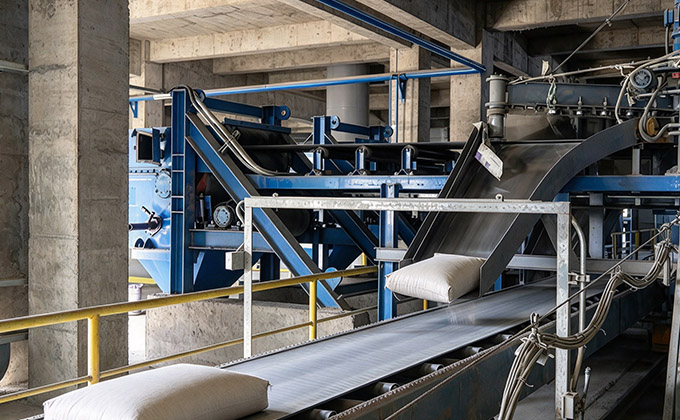
Automated material flow, dust management, bulk loading and remote valve control reduce strenuous manual labour and human error inside cement facilities. By integrating key equipment such as our air slide conveyors for low-maintenance powder transport, pulse jet dust collectors, cement process valves and automated cement bulk loaders for clean, dust-free tanker filling, cement plants achieve safer working conditions and consistent output quality.
These systems are built for simple daily operation and minimal manual intervention. Optional condition monitoring tools support equipment health tracking and preventive maintenance planning, helping your operations team cut costly unexpected downtime and keep production on target.
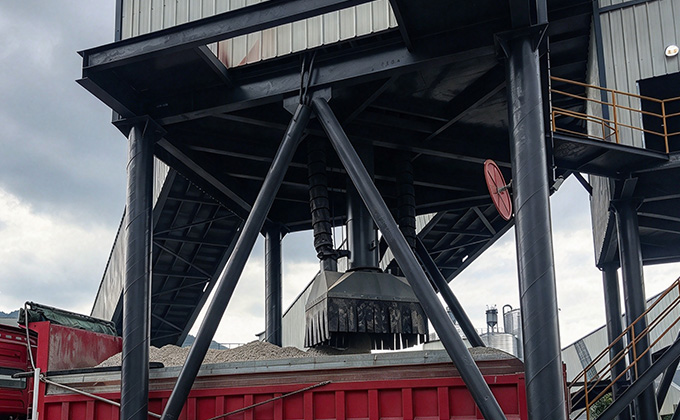
Cement plants require equipment built for long-term reliable operation under extreme site conditions: dust-saturated air, highly abrasive bulk solids, temperature variation and non-stop 24/7 continuous duty cycles. Darko’s cement silo systems, paired with silo discharge activation, flow-control assemblies and wear-resistant process valves, deliver stable material management for open or covered storage yards. Built for extended service life and reduced routine maintenance, these systems guarantee steady, consistent feed to all downstream cement production processes.
For finished cement bulk dispatch, our heavy-duty bulk loading systems — for truck transport and site transfer — are engineered for high throughput while preserving material quality and protecting site safety, even within the most demanding industrial environments.
Common Cement Plant Operational Challenges & Recommended Solutions
- Cement Plant Challenges & Solutions
- Material Selection Guide
| Cement Plant Issue | Recommended Solution | Darko Typical Equipment |
|---|---|---|
| Silo arching / ratholing, unstable powder discharge | Silo fluidization & material activation system | Air slides, aeration pads, flow control valves |
| Heavy dust emission at bulk truck loading | Enclosed dust‑free bulk loading station | Cement bulk loader + local pulse jet dust collector |
| Heavy dust at cement mill and kiln tail | Continuous high-efficiency dust extraction system | Pulse jet baghouse filter |
| Fast component wear caused by abrasive clinker | Wear-resistant conveying system design | Heavy‑duty troughed belt conveyor, hardened industrial valves |
| Frequent blockages at transfer chutes | Optimized chute geometry + flow regulating devices | Custom transfer chutes, modulating control valves |
| Legacy dust collectors failing local emission standards | Dust collection system retrofit and upgrade | New pulse bag filter, full ductwork redesign |
| Material | Core Characteristics | Suitable Darko Equipment |
|---|---|---|
| Finished Cement Powder | Fine powder, prone to arching, high dust generation | Air slide conveyor, cement silo, bulk loader, pulse‑jet bag filter, wear-resistant process valves |
| Raw Meal | Fine powder, moderate abrasiveness | Air slide conveyor, pulse jet bag filter, slide gate valves, diverter valves |
| Clinker | Coarse granular material, highly abrasive, high density | Heavy‑duty troughed belt conveyor, cyclone pre‑collector |
| Fly Ash / Pozzolan | Ultra‑fine powder, low bulk density | Aeration discharge system, cartridge dust collector |
| Slag Powder | Fine, abrasive mineral powder | Air slide conveyor, pulse‑jet bag filter |
Yes. Our engineers assess your current equipment layout, material conditions and emission targets. We deliver targeted retrofits including bag filter replacement, pipeline redesign, silo discharge optimisation, process valve renewal and upgrade of pulse cleaning systems.
Our pulse jet bag filter reaches 99.9% fine particulate capture efficiency. Under cement‑plant high‑dust operating conditions, stable emissions can stay below 10 mg/Nm³.
Generally not recommended. Clinker is coarse and highly‑abrasive while cement powder is fine fluidisable powder. Running both materials on one shared conveyor brings accelerated component wear and increased dust leakage risk. Separate conveying lines are advised.
Core Dust Collection Equipment
-
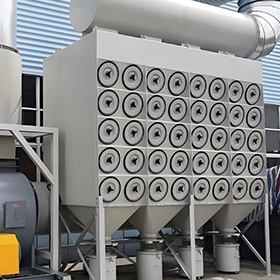
Designed with multi-layered pleated filter cartridges for 99.97% filtration efficiency, optimized for fine particulate control in industries like cement, metalworking, and pharmaceuticals. Compact structure with easy maintenance ensures long-term stable operation.
-
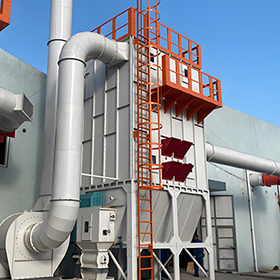
Specifically designed for combustible dust environments with integrated explosion-proof devices and pressure relief systems, compliant with ATEX standards. Perfect for chemical, pharmaceutical, and metalworking industries.
-
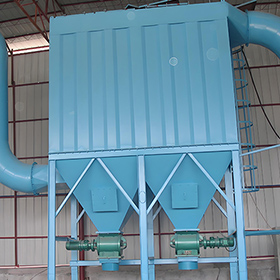
Incorporating advanced pulse-jet cleaning technology for automatic filter maintenance and continuous high-efficiency operation. Offers large air volume capacity with low energy consumption, making it ideal for woodworking and food processing applications.
-
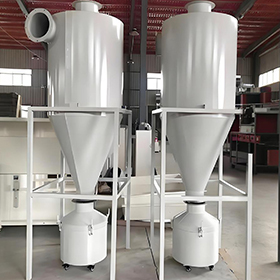
Utilizing centrifugal separation principle to effectively remove large particulate matter. Can serve as pre-filters or standalone units with simple structure, no consumables, and low operating costs – excellent for primary dust collection needs.
What We Can Deliver
Darko offers flexible service models to match different cement‑project requirements:
- Full Turn‑key Solutions Complete engineering, manufacturing and commissioning guidance for new cement grinding plants or full‑scale cement production lines.
- Existing Cement Line Retrofit & Upgrade Energy‑saving transformation, ultra‑low‑emission upgrade, capacity expansion and automation improvement for operating cement facilities.
- Standalone Equipment Supply Individual dust collectors, conveyors, ball mills, cement silos, bulk loaders, cement process valves and comprehensive spare‑part packages.
- Full Lifecycle Support On‑site consultation, process design, manufacturing, installation guidance, commissioning, operator training and long‑term spare‑parts supply. Our global‑focused service team supports cement projects worldwide and helps plant operators minimise unplanned production downtime.
Silo arching is a frequent challenge for fine cement‑based powders. We design silo aeration fluidisation systems combined with flow‑control valves to activate material and guarantee smooth, stable discharge performance.
Yes, we provide full‑range spare parts for dust collectors, conveyors, ball mills, bulk loaders, silo‑related accessories and cement process valves.